描述
I. Applications
The SL20X Series Bearing Heateris mainly used for heating various metal components such as bearings, gears, couplings, railway locomotive wheel centers, wheel tires, and other interf403号即梦图erence-fit components. Heating causes the workpiece to expand, providing the required clearance for interference-fit assembly or disassembly.
II. Advantages
Many bearings are damaged during installation, and improper heating methods are one of the main causes.
Heating with welding or flame tools may cause bearing deformation.
Furnace heating may result in uneven heating on different sides of the bearing.
Oil-bath heating may contaminate bearings if the oil is not clean, resulting in increased operating noise.
Oven heating requires a relatively long heating time.
Hammering bearings into position can easily cause mechanical damage.
The latest induction heating technology used in the ZJ20 Series Induction Heaterprovides the following advantages:
1. Cost Saving
aves up to 90% electricity, eliminates 100% of oil consumption, and reduces required workshop space by approximately 70%.
2. Time Saving
mproves working efficiency by more than 4 timesand can reduce operator requirements by approximately 80%.
3. Reliable Heating
rovides uniform and completely clean heating, helping improve assembly quality.
4. Safe Operation
liminates the fire hazards associated with flame and oil heating methods.
5. Environmentally Friendly
o oil fumes or fuel contamination, helping improve the working environment and operator health.
III. Structure
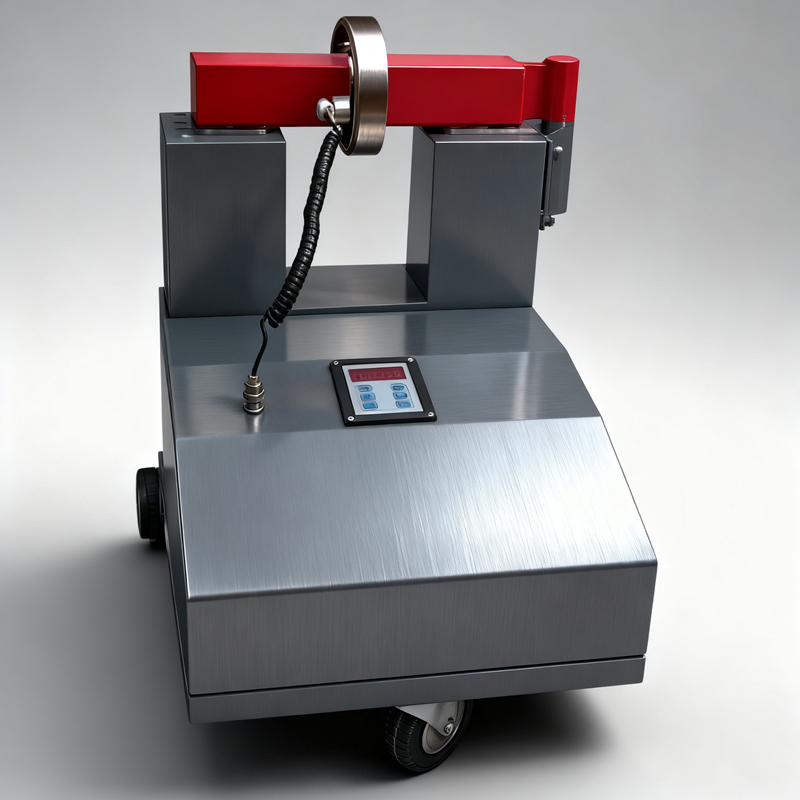
The ZJ20 Series Heaterconsists of a dry, self-cooling, power-frequency induction heating unit (hereinafter referred to as the main unit) and a control system.
Models ZJ20Xand ZJ20Tare mobile units, while the other models are designed as stationary units.
IV. Working Principle
1. Short-Circuit Heating
The main unit functions as a specially designed transformer. A removable yoke passes directly through the bearing or other workpiece to be heated.
When the main unit is energized, the workpiece acts as the secondary winding of the transformer. A high induced current is generated within the workpiece, causing it to heat rapidly.
2. Eddy-Current Heating
The workpiece and the iron core of the main unit form a closed magnetic circuit.
During operation, magnetic flux from the main unit passes through the workpiece, generating eddy currents that rapidly heat the workpiece.
V. Installation and Commissioning
1. Place the yoke securely on the end face of the main unit’s iron core.
2. Check that the wiring of the plug and socket is correct and ensure that the equipment is properly grounded. Insert the plug into a power outlet equipped with a control switch.
3. Set the function selector switch to Manual Control, then switch on the power supply. The red indicator light will illuminate.
4. Press the Startbutton. The main unit will energize, the green indicator light will illuminate, and the red light will turn off. Press the Stopbutton; the red light will illuminate and the green light will turn off.
The commissioning procedure is now complete and the heater is ready for operation.
VI. Operating Procedure
1. Select the appropriate yoke according to the inner diameter of the bearing (refer to Table 2). Place the bearing onto the yoke, then position the yoke securely and evenly on the end face of the main unit’s iron core.
2. During heating, use a temperature measuring instrument to monitor the temperature rise at the end face of the bearing inner ring. When the required temperature rise is reached, record the heating time, stop the heating process, remove the yoke, and take off the bearing for assembly.
3. When continuously heating bearings of the same specification, set the function selector switch to Time Controland preset the required heating time. The power supply will automatically shut off when the preset heating time is reached.
4. After operation is completed, set the function selector switch to the Stopposition and disconnect the power supply.